Leading a new era of intelligent warehousing
Founded in 1806 and headquartered in New York, USA, Colgate is dedicated to improving consumers' quality of life through innovative products and quality services. Its signature red, white and blue colors and its brand concept of "a healthy smile every day" are deeply rooted in people's minds, helping it become a household-name personal care giant.
As the world's leading manufacturer and supplier of toothpaste, toothbrushes and oral care products, Colgate always puts consumer health and satisfaction at its core and attaches great importance to every step that brings a product into consumers' hands. From product research and development to manufacturing and on to final warehousing and transport, Colgate has always held to an attitude of striving to be the best.
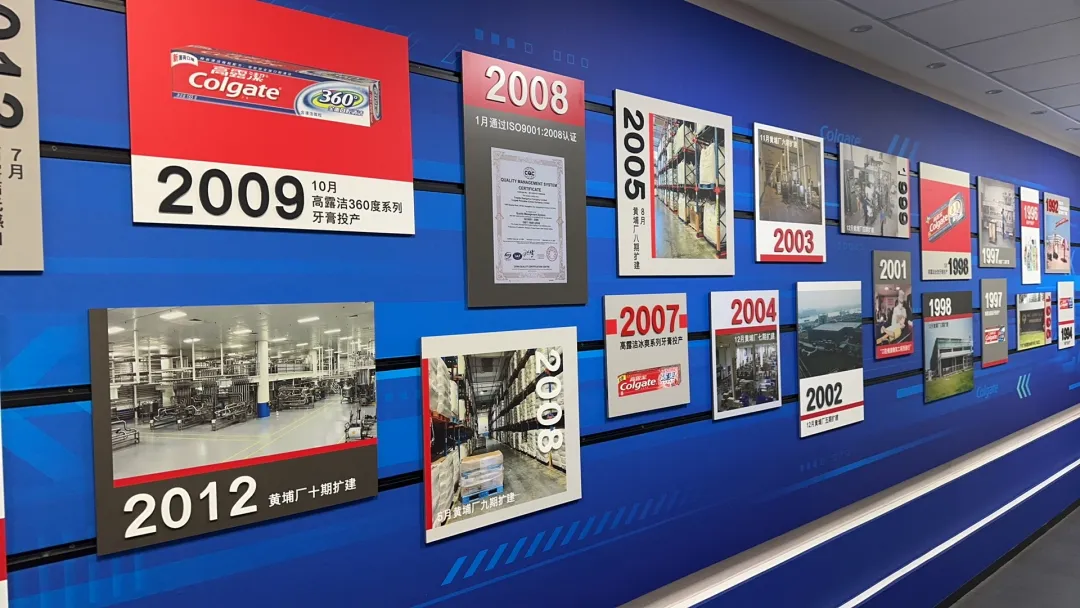
As market demand keeps growing and the business continues to expand, the existing conventional operating model of high-bay racking plus forklifts can no longer meet Colgate's current operational requirements, and improving warehouse management efficiency is a problem Colgate faces and urgently needs to solve. Drawing on its deep technical foundation and extensive industry experience, ATOMIX created a tailored intelligent warehousing solution for Colgate, upgrading the Colgate warehousing system in Guangdong.
Intelligent solution boosts operational efficiency
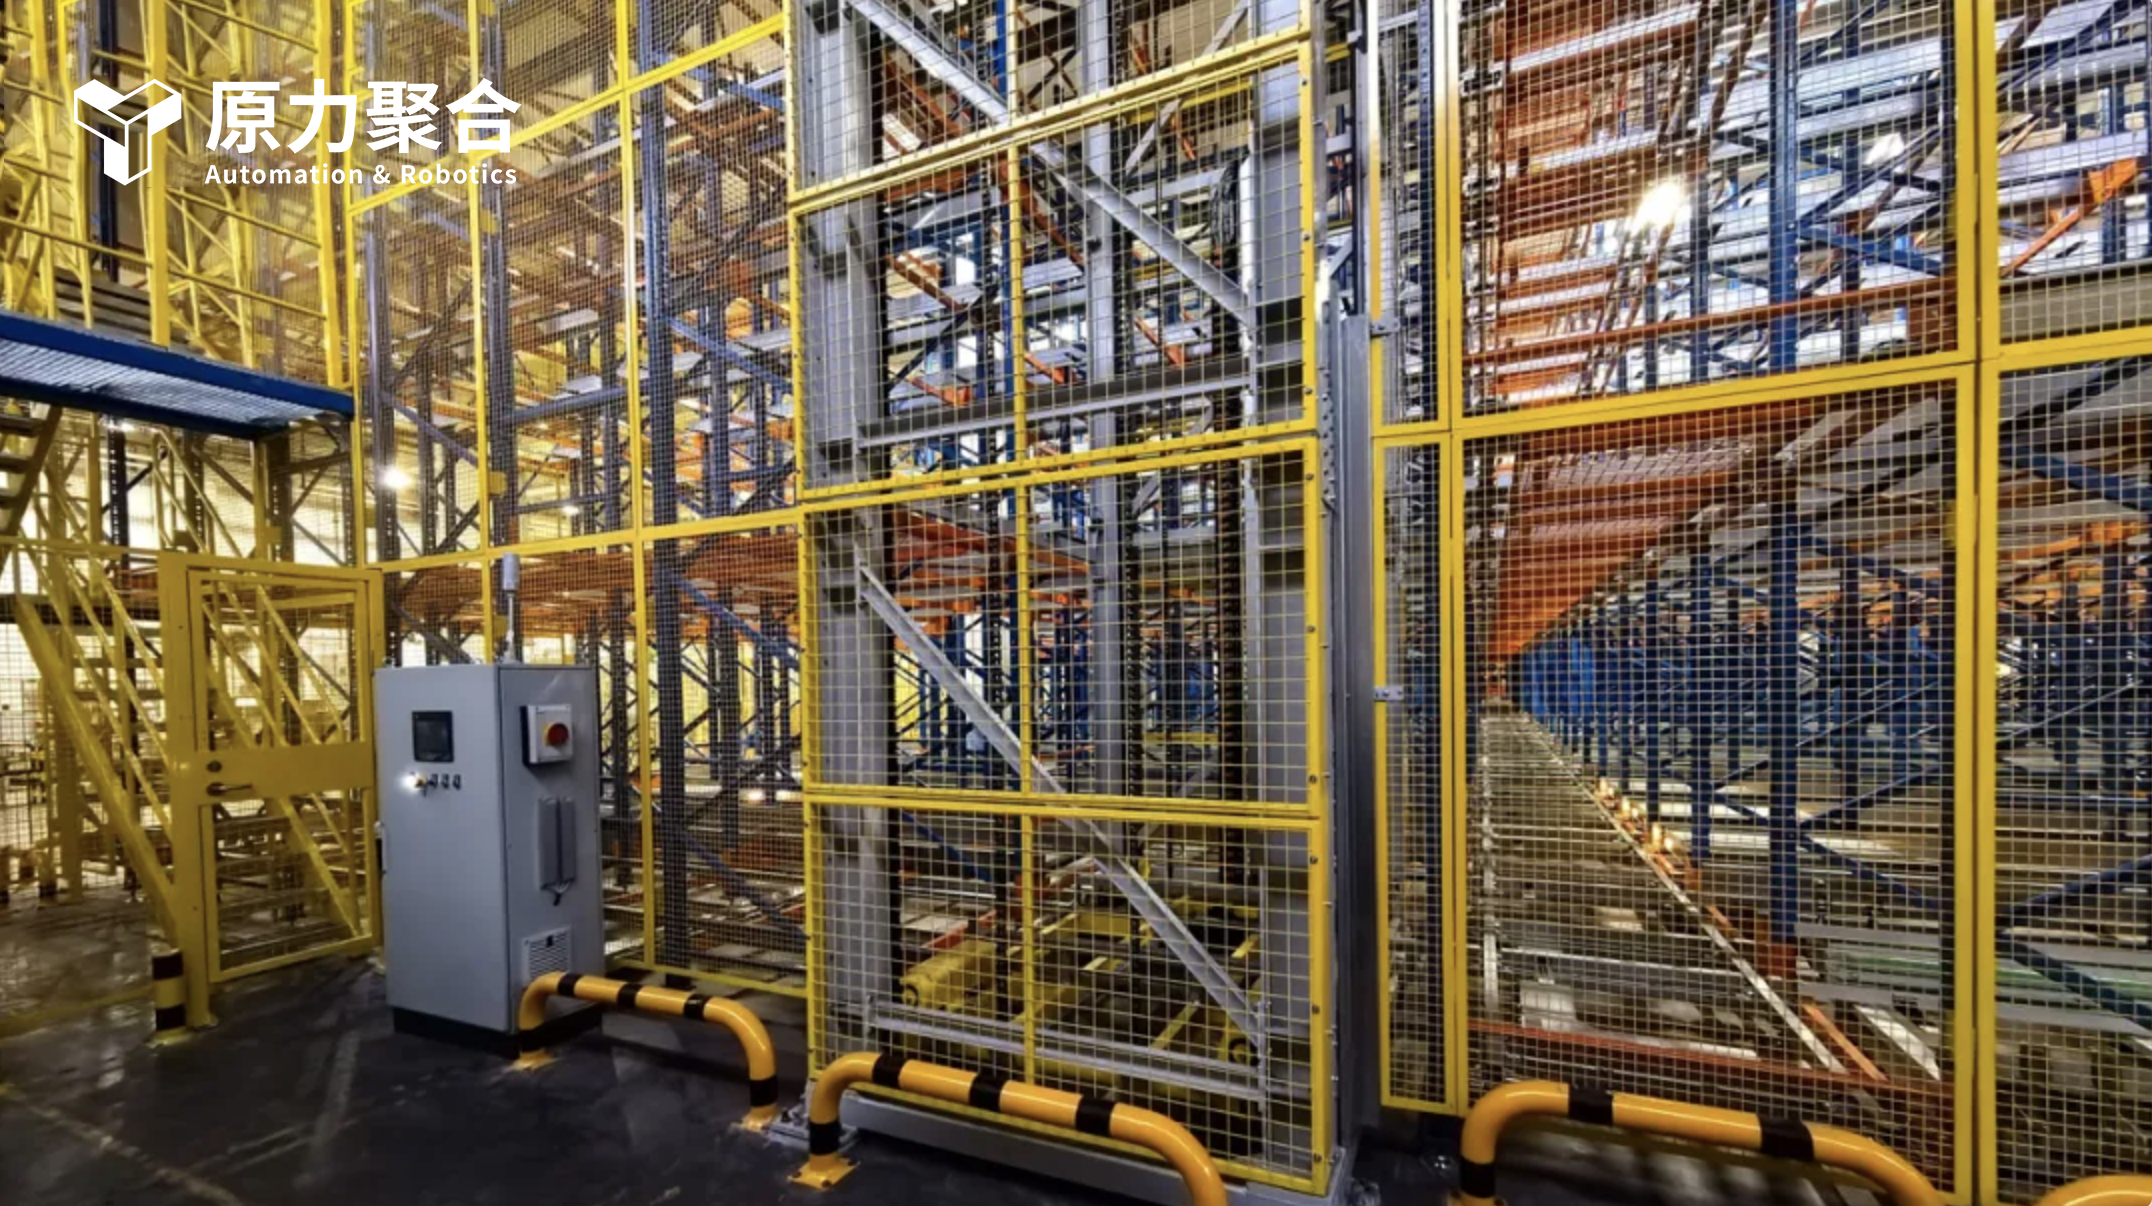
The Matrix 8 Storage pallet shuttle intelligent storage and retrieval solution ATOMIX customized for Colgate is one of the three subsystems of ATOMIX's Matrix 8 integrated solution. It incorporates advanced AI algorithms and brings together the four-way shuttle system, the lift system, the pallet conveyor system and the racking system, realizing intelligent, unmanned management of the entire process from inbound receiving and storage to outbound retrieval, with the characteristics of high density, flexibility and scalability.
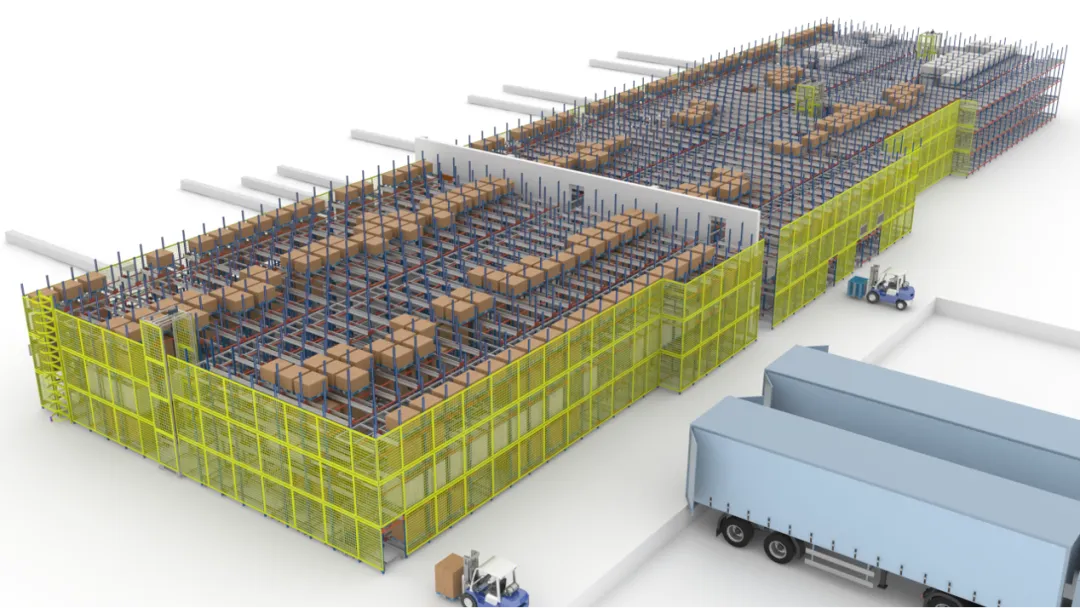
Thanks to the powerful AI algorithm optimization capabilities of the intelligent software system, ATOMIX's Matrix 8 Storage subsystem can achieve high-density storage while easily handling scenarios with many SKUs and high throughput. Compared with the previous conventional warehouse, the overall turnkey solution provided to Colgate raised overall efficiency by 30% and achieved 20% growth in storage capacity.
Innovative solution reshapes customer warehouse management
01 Lower labor costs
The intelligent four-way pallet shuttle warehouse solution enables unmanned warehouse operations, replacing the traditional forklift handling step Colgate used before, saving a large amount of manpower and reducing warehouse operating costs.
02 Maximize warehouse space utilization
In Colgate's warehouse, the Matrix8 Storage solution uses optimized algorithms and data analysis to arrange cargo storage locations rationally, improve the utilization of warehouse space and achieve 20% growth in storage capacity.
03 Improve inventory management accuracy
Changing the past situation of numerous product categories and complex inventory management, Matrix8 Storage can monitor and record the inbound and outbound movement of goods in real time, providing accurate inventory data and analysis.
04 Greater order flexibility and faster response
The intelligent four-way shuttle system solution provided by ATOMIX helps Colgate achieve fast order processing and flexible goods scheduling, ensuring that Colgate can meet customer demand in a timely manner and improve customer satisfaction.
05 Ensure supply chain stability
The introduction of the intelligent four-way shuttle system helps Colgate reduce uncertainties in the supply chain, guarantee timely delivery of goods and maintain stable supply chain operations.
AI algorithms solve thorny problems
01 Solving uneven floor load capacity in the old warehouse
The floor load capacity of the old warehouse is far below that of a newly built warehouse. To solve the problem of uneven floor loading, ATOMIX uses AI algorithms to monitor and calculate the load conditions in each area of the warehouse in real time, dynamically and evenly distributing pallets of different weights to different areas of the warehouse, ensuring balanced loading within the warehouse and effectively preventing problems such as floor settlement.
02 Connecting the production workshop and the dock to shorten transport distances
Through the integrated through-passage design of the conveyor line within the four-way shuttle racking, the production workshop and the dock are connected, which shortens transport distances and greatly improves transport efficiency while also ensuring maximum storage capacity.
This collaboration is an important exploration and practice by Colgate and ATOMIX in the field of intelligent warehousing. It not only sets a benchmark for the intelligent transformation of the personal care industry, but also enables Colgate to better respond to future changes in consumer demand and continue to maintain its leading position in the industry.
In the market environment, ATOMIX will always adhere to being technology-driven, providing customers across industries with more valuable solutions and helping them keep moving forward on the path of digital transformation. In the future, both parties will continue to work hand in hand to explore more possibilities of intelligent technology and write a new chapter in logistics management.